Overview
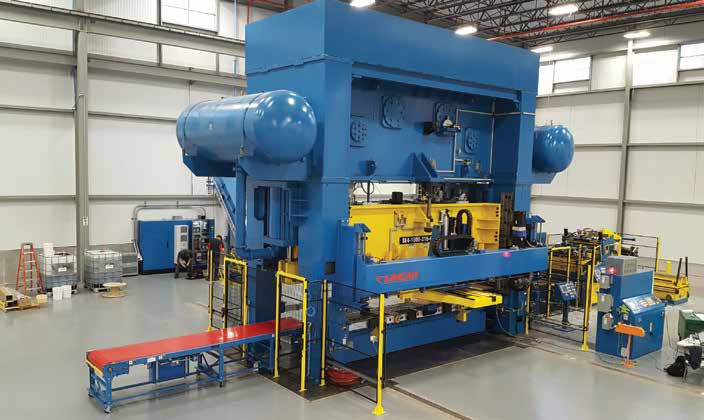
Linear servo transfer systems move parts from station to station in a transfer die, with every axis under servo control for fast, accurate, fully programmable motion. Linear builds front-and-rear, window-mounted and bolster-mounted transfers, so there is a fit for presses with small windows, large windows and compact bolsters, on new presses or as a retrofit.
Key Features
- Front and Rear (FR) series
- Mounts on the front and rear of the press, so it retrofits presses with small or no windows. Independent motion on the front and rear units and infinite pass-line adjustment.
- Wide-body (FRW) and FR4P series
- FRW covers larger presses. FR4P handles larger payloads and bolsters, with dual transfer units per side, and retracts up and out of the way when the press runs without the transfer.
- Multi-directional (MD) option
- Adds multi-directional transfer motion, with production in left-to-right or front-to-back configurations.
- Window Mounted (WM) series
- Mounts through the press window. Suited to presses with large windows or sound doors, with better die visibility and a smaller front-to-back footprint.
- Small press solutions
- Bolster-mounted transfers and gap frame transfer lines for compact presses.
- Tooling and simulation
- Linear designs the end-of-arm tooling (receiver style, sub-rail or fixed), runs a full 3D transfer simulation with guaranteed run rates, works directly with the die shop and provides the 3D tooling data.
Product Line / Models
Linear's transfer families:
- FR / FRW – front and rear mounted, standard and wide body.
- FR4P – larger payloads and bolsters, dual units per side; MD multi-directional option.
- WM – window mounted, for presses with large windows or sound doors.
- Bolster-mounted and gap frame lines – for compact presses.
Applications & Benefits
- Progressive to transfer: Transfer dies carry parts with fingers instead of a carrier strip, which can save material and allow more complex parts.
- Retrofits: FR and WM transfers mount to existing presses.
- Faster start-up: Simulation and tooling design before the die arrives cut start-up time and protect run rate.
- Flexible changeover: Programmable strokes and stored recipes for each job.
How to Choose the Right Linear Transfer
- Press type, tonnage, bolster size and window size.
- Part size and weight, and the number of die stations.
- Whether the press also needs to run progressive dies (retractable or removable transfer).
- Blank feeding and part unloading needs at each end of the press.
Why Linear Transfers Are Trusted
- Built for stamping: Linear started in 1994 building transfer systems for metal stamping and now supplies transfer, front-of-line, end-of-line and press-to-press automation worldwide.
- In-house from design to start-up: design, programming, assembly, installation, commissioning and training are all done by Linear.
- Supported in North America: Linear is part of Nidec Press & Automation, with service locations in Barrie and Windsor, Ontario, Louisville, Kentucky and Monterrey, Mexico, and 24/7 support.
Contact & Ordering
Need help picking the right model or getting a quote? Provide these details:
- Press make, model, tonnage and bolster size
- Window dimensions and pass line
- Part print or sample, part weight and number of stations
- Target strokes per minute
- Contact PRI to discuss specs, lead times, and installation support.