
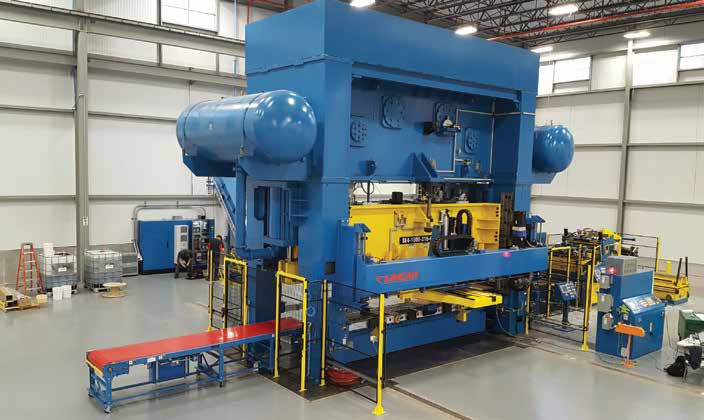
Linear Automation, a Nidec Press & Automation company, builds the automation around a stamping press: servo transfers, blank destackers, end-of-line stacking, press-to-press lines, turnkey cells, custom robotic and vision cells, control upgrades and IRIS monitoring. Production Resources, Inc. (PRI) represents Linear and helps you scope the job.
Shop Press Transfer AutomationRequest a QuoteCall (800) 863-3164What Linear Builds · Tooling & Simulation · Service · Where to Start · What We Need · Brands · FAQs
What Linear Builds
Linear has built press and factory automation since 1994. It started with transfer systems for metal stamping and now covers the whole line, from the blank stack to the finished-part rack, plus automation outside the press room. Design, programming, assembly, installation, commissioning and training are done in-house. For the company background, see the Linear line card.
In a stamping line, blanks come in at the front, a transfer or press-to-press system moves the part through the dies, and end-of-line automation takes it away. One control point can run the press, the transfer and the automation. Pick a card to read more, or go straight to the catalog.
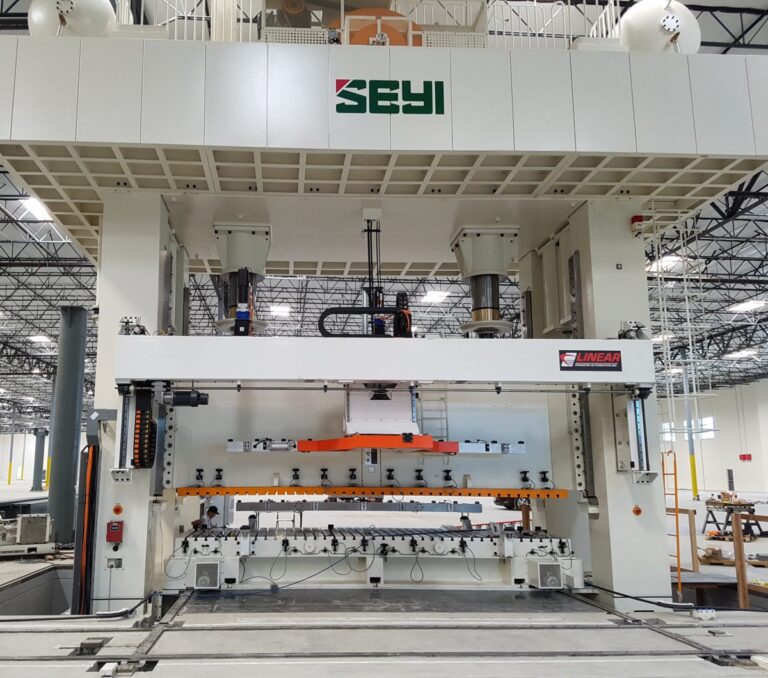
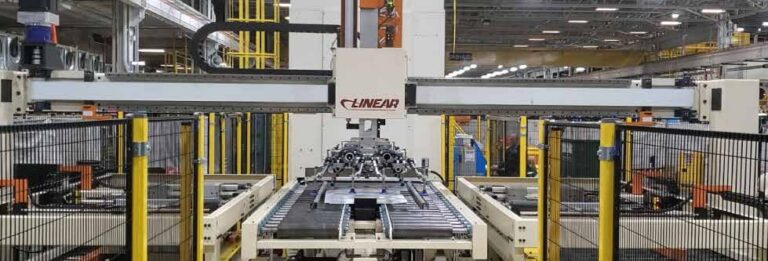
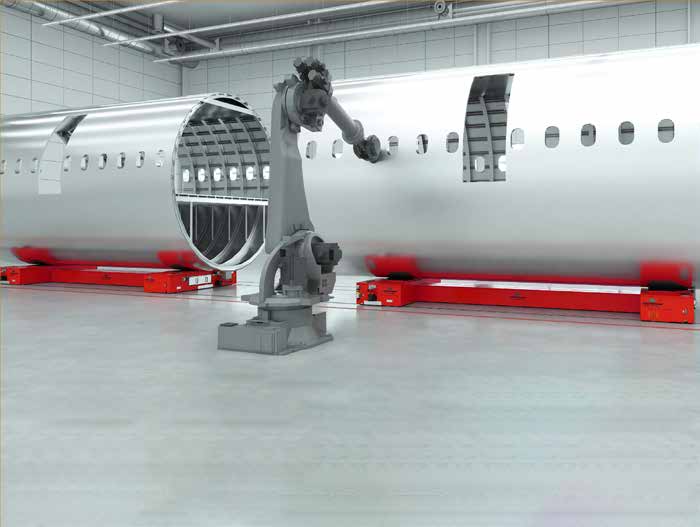
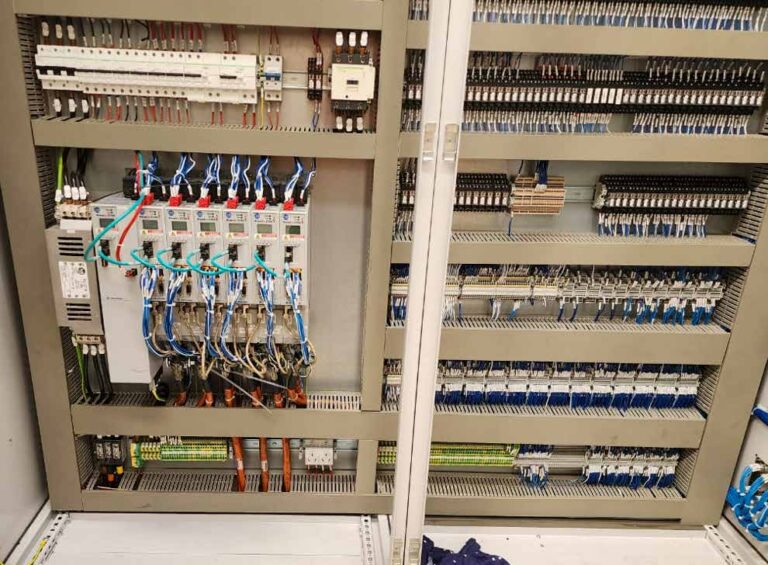
The control upgrades help older presses meet current OSHA, ANSI and CSA requirements, and add single-point line control, quick die change and ADC sequencing, and integration of feeds, destackers, robots, conveyors, racking and scrap systems. Linear offers three levels of support on a control project: Linear installs and commissions everything; you install and Linear commissions on site; or you install and commission with Linear's phone support.
Tooling and Simulation
Linear designs the end-of-arm tooling for its transfers and automation: receiver-style, sub-rail and fixed tooling systems, with fingers, grippers, suction cups, floater bases, vacuum generators, and double blank and part-detect sensors. It can use the components you prefer, works directly with your die shop, runs a 3D transfer simulation and a run rate analysis before the die is built, and supplies the 3D tooling data with the package.
For the tooling components themselves (receivers, modular fingers, grippers, shovels and vacuum cups), see the Norgren transfer tooling guide. Linear's Paul Stirrett covers what makes a transfer launch go smoothly in Keys to Success When Launching a Transfer Job.
Linear Service and Support
Linear supports its own systems, and other makers' equipment, from five service locations: Barrie and Detroit-Windsor in Ontario, Louisville, Kentucky, Monterrey, Mexico and Bangkok, Thailand. The service team is available 24/7.
Where to Start
- 1Start with the part and the pressPart size, weight and material; the die (progressive, transfer or line dies); the press make, tonnage, bolster and window size; and the target strokes per minute.
- 2Decide how parts move through the pressA servo transfer for a transfer die in one press, press-to-press or crossbar automation for a line of presses, or a robot cell. The press transfer guide covers how to choose a transfer.
- 3Decide how blanks get inCoil-fed, or blanks from a destacker. Blank size, weight and material (steel, aluminum or coated) set the destacker, and double blank detection protects the die. Blank feed can share a cell with a coil feed line.
- 4Decide how parts get outAn exit conveyor to manual racking, robotic racking and stacking, or in-line inspection. Rack type, part orientation in the rack and line speed decide it.
- 5Plan the controlsSingle-point line control, recipes by job, quick die change sequencing, die protection and safety. Linear works on Allen-Bradley, Siemens, Bosch and Mitsubishi platforms and five robot brands, so the line can follow your plant standard.
- 6Plan support from day oneTraining, spare parts and service after startup, and whether you want IRIS monitoring on the new line.
Send what you have. Part drawings and a floor layout go a long way:
- Part drawings or 3D models, weights and material
- Die type and number of stations
- Press make, model, tonnage, bolster and window size
- Target strokes per minute or parts per hour
- Coil or blank fed, and blank sizes
- How finished parts leave: rack, container or conveyor
- Floor space and a layout drawing
- Plant standard PLC and robot brands
- New line or retrofit, and your timeline
Brands PRI Pairs With Linear


Help From PRI
Local: PRI is based in Franklin, Tennessee, and brings Linear's engineers to your plant. Application help from the start: PRI looks at your parts, presses and floor space first, so the quote fits the job.
One partner for the whole press room: PRI can put Linear automation together with Norgren transfer tooling, Wintriss controls and die protection, PAX lubrication, MPI conveyors, Pascal quick die change and Stamtec presses on one project. PRI supports the installation and startup, operator training and parts, and its safety surveys and stop-time measurements help you place guarding around the automated line. See PRI services.
Linear Downloads
Frequently Asked Questions
What does Linear Automation make?
Servo transfer systems, blank destackers and front-of-line automation, end-of-line stacking and racking, press-to-press and crossbar automation, turnkey stamping cells and press lines, custom robotic and vision cells, AGVs, PLC press and automation control upgrades, and IRIS equipment monitoring.
Can a Linear transfer be added to an existing press?
Yes. The FR series mounts on the front and rear of the press and retrofits presses with small or no windows. The WM series mounts through the window on presses with larger windows or sound doors. Bolster-mounted transfers suit compact presses.
What is the Strothmann agreement?
Strothmann Machines & Handling builds high-speed tandem line feeders and crossbar automation. Linear has an exclusive technology agreement for Strothmann's crossbar and tandem press line automation in North America, including the FeederPlus6neo feeder and the High-Speed Crossbar.
Does Linear support equipment it didn't build?
Yes. Linear's service team supports Linear and non-Linear equipment, and Linear installs, services and upgrades Wintriss press control systems.
What is Linear IRIS?
IRIS (Intelligent Reporting Information System) is Linear's Industry 4.0 line for new or existing equipment. It can read data from existing components, upgrade components for better diagnostics, or add sensors, and it has predictive maintenance, equipment monitoring and production reporting modules. The OEE guide compares it with Wintriss ShopFloorConnect.
How do I get a quote on Linear automation?
Contact PRI with your part, press and rate. PRI and Linear's engineers scope the job, and PRI quotes it.
Related Guides
Power Press Transfer Systems · Norgren Transfer Tooling · Bachhuber Press Unloaders · Assembly Automation · SmartPAC PRO Press Automation · OEE & Production Monitoring · Coil Handling & Feeding · Power Presses · Quick Die Change
Send us the press, the part and the rate you need. PRI will bring in Linear's engineers and quote the automation that fits.
Shop Press Transfer AutomationRequest a QuoteCall (800) 863-3164